A metal shelving unit’s load rating is useful only with the configuration and loading conditions behind it. Buyers also need to know whether production units assemble correctly, stay stable in their intended use and arrive with the specified hardware and finish. A neatly assembled display rack cannot answer all of those questions.
For a practical metal shelving quality inspection, assemble units from production cartons, check their parts and joints, then assess load resistance and stability under the approved test conditions. Inspect coating and packing alongside those functional checks. The guide below focuses on manually assembled, floor-supported shelving; installation engineering and operating inspections for industrial pallet-racking systems require a different assessment.
Five Checks to Include in a Metal Shelving Inspection
- Load distribution: Apply the agreed masses at the specified shelf levels and positions. Measure bending during loading and remaining deformation after unloading. Compare with the model’s load limits and deformation criteria; inspect supports and joints for damage or movement.
- Stability: Use the specified floor, shelf arrangement and restraints. Check rocking, sliding, lifted feet and tipping under the approved loading sequence. Judge each applicable observation against its criterion. Supporting weight does not establish resistance to tipping.
- Hardware and connectors: Count and identify bolts, nuts, washers, clips, couplers and caps against the exact model’s parts list. Correct quantities, dimensions and versions; parts fit and engage as intended.
- Coating and edges: Inspect exposed surfaces, joints, welds, cut edges and packed contact points; perform specified coating tests where suitable. Appearance and workmanship meet the agreed defect criteria; measured coating results meet their separate requirements.
- Assembly and packing: Follow the retail instructions with the specified tools. Check shelf seating, alignment, labels and carton protection. Assembly works without undocumented substitutions or forcing; the packed contents match the ordered configuration.
Before inspection, add the actual test masses, placement, duration, measurement points and acceptance limits to the schedule. If a load claim has no supporting method or criteria, an inspector can report observations but cannot turn an improvised demonstration into validation of that claim.
Start with a Boxed Unit and the Correct Parts List
Open selected production cartons and identify the shelf version before counting parts. Compare fastener diameter and length, connector geometry, support members, shelf panels, caps and any specified restraints with the drawing and approved sample. Equal quantities do not establish that the factory packed the correct hardware: a shorter bolt or different clip may fit into the bag yet fail to make the intended joint.
For boltless shelving, inspect the connectors that replace threaded fasteners. Rivets, slots, clips and post couplers still need the specified engagement. Edsal’s MuscleRack wire-decking shelving uses a rivet-lock construction with post couplers. The same product page lists 1,000 lb per shelf and 5,000 lb for the unit, both with evenly distributed weight. These are manufacturer ratings for that construction, not acceptance loads for another supplier’s rack.
Assemble with the retail instructions and named tools, recording any step that requires knowledge absent from the manual. Check that beams and shelf supports engage fully, shelf panels seat correctly and any diagonal bracing or other stabilizing members are installed as specified. Compare assembled height, width, depth and shelf positions with the drawing. Record elapsed assembly time if it is an agreed requirement, identifying the tools and assembler’s familiarity so the comparison is meaningful.
Check the drawing revision as well as the model name. A manufacturer’s WEB674 assembly manual, for example, provides a parts list and a defined sequence for building its wire shelving. Obtain that level of detail for the ordered product. A generic carton photograph cannot identify a missing support or explain the intended position of a connector.
Keep the first assembly observation before a factory technician corrects it. A unit that only becomes usable after an undocumented adjustment presents a different customer problem from a unit that assembles correctly from the box. Photograph the joint before intervention and state what changed.
Match the Load Test to the Shelf Rating
A uniformly distributed load is weight spread across the intended shelf area rather than concentrated at one point. That loading condition matters to both the shelf panel and its supports. A heavy object placed at the center does not reproduce an evenly spread loading arrangement, even when the total mass is the same.
Confirm both the per-level limit and the whole-unit limit, along with the configuration to which each applies. Do not derive an approved total capacity simply by adding shelf labels. Ask whether the supporting test covered the actual shelf span, panel, reinforcements and connection version being ordered.
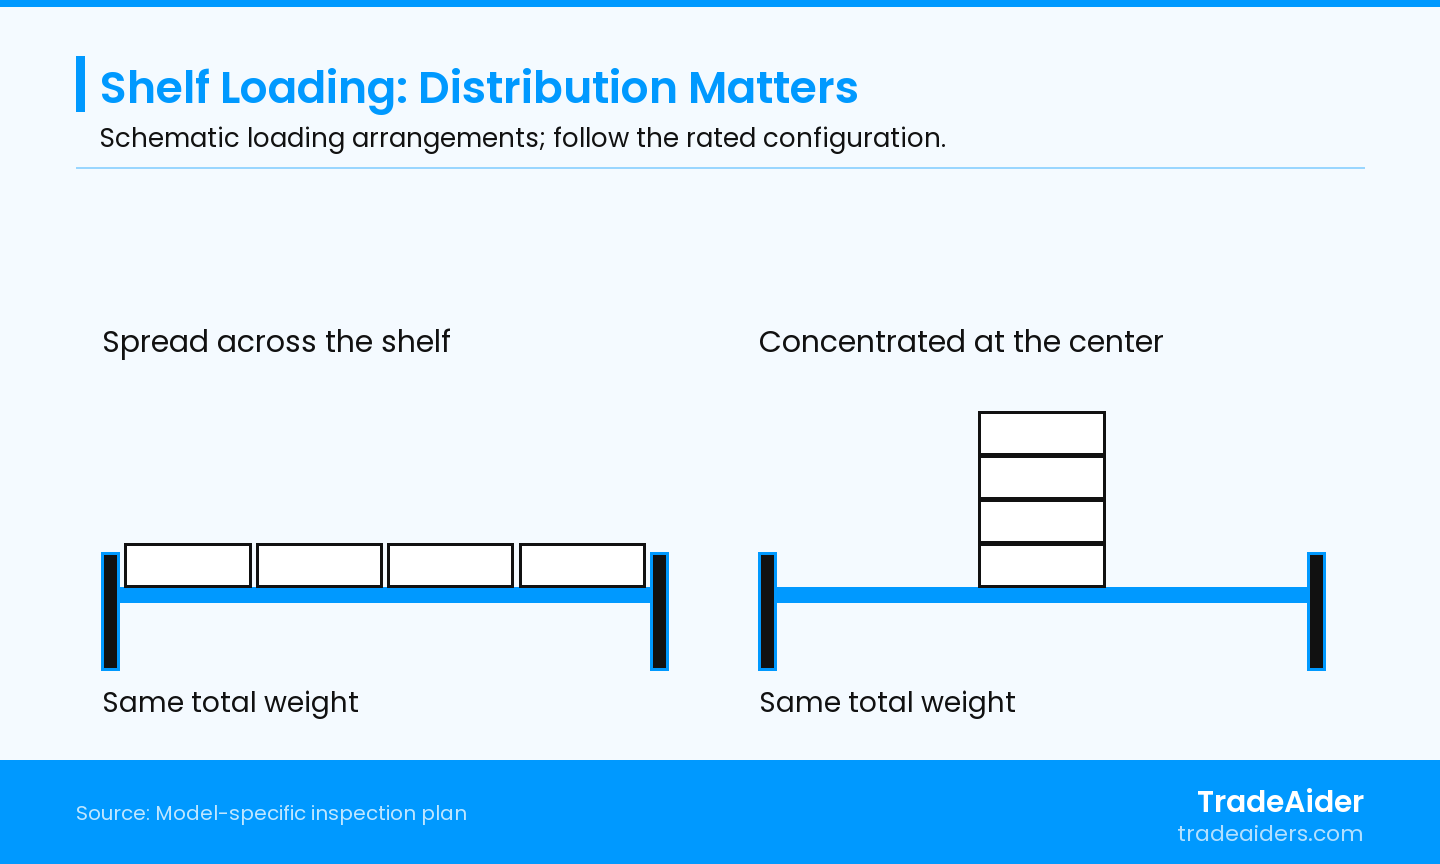
Schematic comparison, not a test result: equal total weight does not reproduce the same loading condition. Use the distribution specified for the rated model.
Use weighed masses and a controlled setup approved by the testing party. Record the shelf levels, load placement, total mass and mass by level, duration and support conditions. Measure deflection, meaning displacement under load, at the specified points. After unloading, check residual deformation, meaning the shape change that remains, together with cracks, loosened connections, shifted supports or permanent bends.
A useful load-test record identifies the unit and shelf, the initial measurement, the reading while loaded, and the reading after the specified recovery period. Include the mass placement photograph and the applicable limit beside the result. If loading equipment spreads the weight through a plate, record that plate and its contact area: the setup should reproduce the prescribed distribution, not unintentionally strengthen the shelf.
The distinction between temporary bending and a permanent change helps the supplier investigate the result. If a shelf remains bent, retain its identity and inspect the panel, span and supports; do not report only “load test failed.” Conversely, a shelf that recovers its shape may still fail an agreed in-load deflection limit. Compare each required measurement with its own criterion.
Do not choose an overload factor or test duration at the factory because another product uses it. Structural qualification of a claimed capacity needs an appropriate engineering method; routine inspection checks whether sampled production units meet the agreed requirements. Use trained personnel and controlled loading, keep people away from potential falling loads, and segregate units damaged by testing.
Check Stability in the Intended Configuration
Shelving stability concerns how the complete assembled unit behaves on its supporting surface, not just how much weight a shelf carries. Start by checking foot contact and alignment on the specified floor. Rocking from an uneven foot, sliding across the surface and tipping are different observations, so identify the movement instead of grouping all of them under “wobble.”
Follow the approved stability method, including shelf heights, permitted uneven loading, load positions and any specified applied forces. Document required wall or floor restraints and how they are installed. A restrained unit and an unrestrained unit are different test configurations; an improvised strap should not conceal a problem or replace the intended installation.
Changing the feet can change the usable rating. Seville Classics lists its WEB674 shelving capacities as 1,200 lb for the complete unit on leveling feet, compared with 110 lb on wheels. These figures apply only to that model; they illustrate why a report for the fixed-foot arrangement cannot automatically substantiate the wheeled version. Match the base hardware and configuration before comparing results.
When the result changes, compare the floor and setup before attributing it to improved production. Then inspect feet, joints, bracing, shelf engagement and the actual component version. Moving weight lower or changing shelf positions may alter the behavior, but such an adjustment is acceptable only when it belongs to the approved use configuration. It does not establish that the original advertised arrangement passed.
Inspect the Finish Where Damage Is Easy to Miss
Examine beam ends, welds, punched slots, tube interiors where accessible, cut edges and surfaces that touch inside the carton. Record rust, bare areas, burrs, coating runs, flaking and scratches by location and effect. A mark on a hidden surface may differ from a sharp edge encountered during assembly; use the buyer’s defect examples rather than assigning every surface fault the same severity.
Appearance, coating thickness and adhesion—the coating’s attachment to its substrate—are different characteristics. Where cured-coating thickness is specified, use a suitable instrument and the agreed measurement locations. For an adhesion rating, ASTM D3359-23 covers tape applied and removed over cuts in applicable coating films on metallic substrates. It does not provide an absolute bond-rupture force. Confirm method suitability, coating thickness, trained operation and the required rating instead of calling an arbitrary tape pull a standardized test.
If corrosion performance is part of the purchase requirement, match the report to the ordered material and coating system. ASTM B117-26a specifies the salt-spray test environment and procedures, but does not set a product’s exposure period or interpretation of results. It also cautions against predicting natural-environment performance from salt-spray results alone. Specify the exposure and assessment criteria separately; do not convert chamber hours into a promised number of outdoor service years.
Separate sorting decisions from longer performance investigations. A repeatable scratch at the same packed contact point calls for checking separators and movement between parts. Peeling near welds calls for examining coating attachment and the affected production scope. Photographs should show both a close view of the defect and its position on the component, so the supplier can investigate the right operation.
Check the Product Inside the Carton
Verify the assortment, model labels, instructions, hardware packets and protection of long members, corners and coated surfaces. Check whether components can rub together or move during the specified handling sequence. After any agreed package test, inspect shelf seating, connectors and relevant product functions as well as the box. A clean outer carton does not show whether an internal support has bent.
Use the TradeAider inspection standard when discussing the sampling and defect-reporting arrangement, then add the shelving-specific methods. State how many units will be assembled or allocated to load and coating tests. Those allocations need not equal the visual-workmanship sample, and a lot-acceptance plan does not create a load limit or guarantee that every unit is defect-free.
Agree whether destructive coating checks and structural loading use separate samples. Mark units that have been cut, overloaded or permanently deformed so they are not returned to saleable stock. The report should distinguish results observed before testing from damage introduced by the test itself.
Illustrative Example: All Parts Present, Beams Not Fully Engaged
Consider a hypothetical shipment of boltless shelving. A boxed unit contains the correct parts, but its revised instruction sheet does not clearly show how the beam connections seat in the upright slots. During assembly, the inspector records incomplete engagement and stops before applying the planned load. A technician seats the beams and the corrected unit completes the agreed checks.
The corrected unit’s performance does not erase the original assembly problem. The buyer asks the supplier to compare the instructions with the approved connection geometry and identify stock containing the revised sheet. New instructions are then checked by assembling units from the affected production cartons, without the technician’s undocumented assistance. Where engagement was altered, repeat the relevant functional checks under the approved conditions. This constructed example illustrates why part counts and assembly checks complement one another; it is not a TradeAider customer result or proof that all stock is defective.
Provide the Configuration and Test Schedule Before Booking
TradeAider’s Pre-Shipment Inspection takes place when the order is 100% complete and at least 80% packed. Its published scope includes packaging and accessories, appearance, dimensions and weight, functional checks and a formal report. Agree which shelving checks can be completed during the visit and which require specialist equipment or a longer test period.
Send the approved parts list, assembly drawing, retail instructions, material and coating specification, load-rating conditions, test schedule, defect examples and packing requirements. Include variant quantities and any component or instruction changes. Contact our team to review the inspection scope and quote, so the report can identify the tested configurations, measured results and checks that remain outstanding.
Frequently Asked Questions
Can different shelf widths use the same load report?
Only when the report’s scope actually covers those configurations. A width change can change the span between supports even if the material and finish are unchanged. Compare dimensions, supports, joints, shelf construction and loading conditions, then ask the qualified testing party which evidence remains applicable and which checks need repeating.
Does hardware-packet weight prove the contents are correct?
No. Packet weight may help screen consistency under an agreed process, but different fasteners or mixed parts can have similar total mass. Count and identify sampled contents against the parts list, including the dimensions that affect fit. A weight check should support that inspection rather than replace component identification.
Are unused upright holes always a missing-fastener defect?
No. Adjustable shelving may have unused holes or slots for alternative shelf positions. Compare the assembled configuration with its drawing and instructions to distinguish those positions from a required connection that is empty. Photograph the location and identify the required part before classifying it as missing hardware.
Can a coating scratch be repaired before shipment?
Yes, if the buyer approves the repair method and the finished result meets the applicable requirements. Identify the affected units, repair material and process, then check the appearance and any performance characteristics the repair can affect. A touch-up that hides exposed metal visually does not by itself demonstrate that the specified coating protection has been restored.
Artigos Relacionados
Expanda seu negócio com o Serviço TradeAider
Clique no botão abaixo para entrar diretamente no Sistema de Serviço TradeAider. Os passos simples desde a reserva e pagamento até o recebimento de relatórios são fáceis de operar.